| 1. Furnace Technology and Process Compatibility |
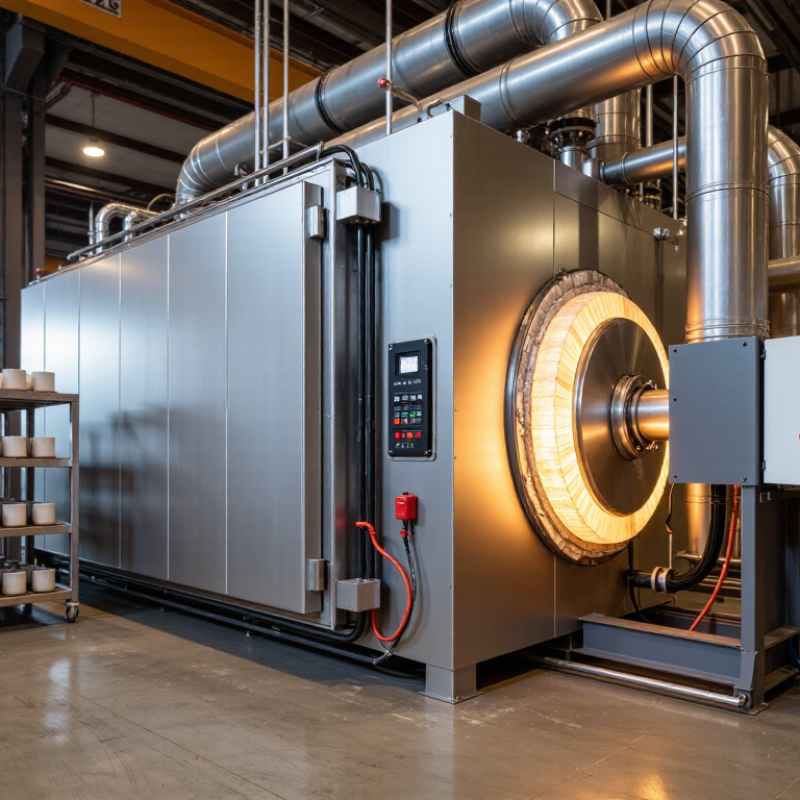
| Primary furnace type | Common options include vacuum sintering furnaces, vacuum-pressure sintering furnaces, low-pressure sintering furnaces, and continuous sintering systems. | The furnace type must match the carbide grade, binder system, product geometry, required density, and production volume. | Process flow diagram, furnace configuration, application list by material type, and sample production results. |
| Suitable carbide process | Cemented carbide is commonly sintered in a controlled vacuum or inert atmosphere. Typical sintering temperatures are approximately 1,350–1,500 °C, depending on composition and process design. | Incorrect temperature or atmosphere control can cause binder loss, abnormal grain growth, distortion, porosity, or cracking. | Validated temperature recipe, atmosphere specification, material compatibility statement, and test report. |
| Maximum operating temperature | Many industrial graphite hot-zone furnaces are designed for temperatures above normal carbide sintering temperatures; the usable process temperature is lower than the nameplate maximum. | A higher maximum rating does not automatically mean better performance. Uniformity, repeatability, and service life are more important. | Rated temperature, continuous operating temperature, heating-element material, and temperature-uniformity test data. |
| Vacuum performance | Vacuum sintering systems are commonly specified by ultimate vacuum, leak rate, pumping speed, and pressure stability. The required value depends on the process recipe and furnace volume. | Stable vacuum conditions help control contamination, binder behavior, and final material properties. | Ultimate-vacuum test curve, leak-rate specification, pump model category, valve arrangement, and acceptance-test procedure. |
| Pressure-assisted sintering | Some systems add inert-gas pressure during the final stage to reduce residual porosity. The exact pressure range must be selected according to the furnace design and carbide process. | Pressure capability is relevant when the buyer requires high density, improved mechanical properties, or reduced internal porosity. | Maximum working pressure, pressure-control accuracy, gas-safety design, pressure vessel documentation, and sample density results. |
| Atmosphere control | Typical process gases may include argon, nitrogen, or other gases specified by the carbide formulation. Gas purity and flow stability should be defined in the purchase specification. | Atmosphere contamination can affect carbon balance, binder phase behavior, surface quality, and furnace components. | Gas-purity requirement, flow-control range, oxygen and moisture monitoring method, and gas-supply interface drawings. |
| Hot-zone construction | Graphite hot zones are widely used for high-temperature vacuum processing. Insulation design, graphite grade, shielding, and replaceable components affect performance and maintenance cost. | Hot-zone design influences energy consumption, temperature uniformity, contamination risk, and replacement frequency. | Hot-zone drawing, material grades, expected service life, replacement-part list, and maintenance instructions. |
| 2. Capacity, Dimensions, and Production Fit |
| Effective working zone | Compare usable width, depth, height, and loading volume rather than only external furnace dimensions. | Usable volume determines the number of trays, plates, or graphite containers that can be processed per cycle. | Dimensioned working-zone drawing, loading diagram, maximum load height, and recommended loading pattern. |
| Rated batch load | Load capacity is normally stated in kilograms and should be separated into product load, graphite furniture load, and total allowable load. | Overloading can reduce uniformity, extend cycle time, and shorten the service life of heating elements and insulation. | Rated product load, total load limit, load-distribution requirements, and performance data at the proposed load. |
| Temperature uniformity | Uniformity should be stated across the qualified working zone at a defined temperature, load condition, and measurement method. | Uniformity affects dimensional consistency, density, hardness, transverse rupture strength, and batch-to-batch repeatability. | Temperature-uniformity survey, thermocouple locations, test temperature, load condition, and acceptance tolerance. |
| Heating and cooling rate | Heating rate depends on furnace size, load mass, hot-zone design, and recipe. Cooling may be natural, controlled, or gas-assisted. | Cycle time and product quality depend on repeatable thermal ramps rather than the fastest empty-furnace rate. | Full cycle chart with an actual load, ramp-rate limits, cooling profile, and guaranteed cycle time. |
| Electrical requirements | Compare rated power, supply voltage, phase configuration, frequency, transformer requirements, and peak electrical demand. | Electrical compatibility affects installation cost, import planning, and factory utility capacity. | Electrical single-line diagram, nameplate data, peak-load calculation, recommended protection devices, and local-grid compatibility statement. |
| Automation level | Control systems may include recipe management, automatic vacuum sequencing, gas-flow control, pressure control, alarm logging, and data export. | Automation improves repeatability and supports process traceability for export-oriented production. | Control-system specification, number of stored recipes, user-access levels, alarm list, data-backup method, and communication protocols. |
| 3. Quality, Compliance, and Supplier Verification |
| Quality-management system | Ask whether the manufacturer operates a documented quality-management system such as ISO 9001. Certification status should be verified with the certificate issuer. | A documented quality system supports controlled design, purchasing, assembly, inspection, and corrective action. | Current certificate, certificate scope, issuing body, validity date, and factory quality procedures. |
| Electrical and machinery safety | Safety requirements depend on the destination market. Buyers may need conformity with applicable machinery, electrical, pressure, and electromagnetic-compatibility rules. | Compliance gaps can delay customs clearance, installation, insurance approval, or site acceptance. | Risk assessment, wiring documentation, safety-circuit description, declarations of conformity where applicable, and destination-market compliance plan. |
| Pressure-system documentation | If the furnace uses pressurized inert gas, the pressure boundary, relief system, inspection method, and local pressure-equipment rules must be reviewed. | Pressure equipment creates additional safety, certification, and installation obligations. | Pressure-vessel documentation, relief-valve specification, hydrostatic or equivalent inspection records, and operating manual. |
| Factory acceptance test | A FAT should verify vacuum, temperature, pressure, alarms, interlocks, cycle operation, and representative loading before shipment. | Testing before dispatch reduces the risk of discovering major defects after international delivery. | Signed FAT protocol, calibrated-instrument records, test videos or reports, punch list, and corrective-action schedule. |
| Reference installations | References should be relevant to the same furnace type, working-zone size, carbide application, and production environment. | Similar operating references provide stronger evidence than general claims or unrelated furnace installations. | Permission-based customer references, application-specific case data, operating duration, and service history. |
| 4. Commercial Evaluation and International Ordering |
| Request-for-quotation content | Include material type, product dimensions, target density, batch mass, cycle target, atmosphere, vacuum, pressure, utilities, destination, and applicable standards. | Complete technical input allows suppliers to quote comparable equipment instead of different assumptions. | Standardized RFQ form, technical datasheet, layout requirements, utility checklist, and list of optional items. |
| Scope of supply | Define whether the offer includes the furnace body, pumps, gas system, cooling system, control cabinet, graphite furniture, spare parts, installation, training, and documentation. | Unclear scope is a common source of unexpected costs and commissioning delays. | Line-item commercial quotation, exclusions list, bill of materials, optional-item pricing, and responsibility matrix. |
| Delivery and installation planning | Lead time varies by furnace size, customization, component availability, testing requirements, and export procedures; it must be contractually confirmed. | Production planning depends on realistic manufacturing, FAT, shipping, installation, and qualification dates. | Milestone schedule covering design approval, fabrication, FAT, shipment, site installation, commissioning, and final acceptance. |
| International trade terms | Specify the agreed Incoterm, shipment port, packaging standard, insurance responsibility, export documents, and destination customs requirements. | Clear logistics terms prevent confusion over freight, insurance, import clearance, unloading, and inland transport. | Pro forma invoice, packing list, country-of-origin document, export classification, shipping dimensions, gross weight, and agreed Incoterm. |
| Payment protection | For large capital equipment, buyers may use staged payments linked to design approval, production progress, FAT completion, shipment, and site acceptance. | Milestone-based payment reduces exposure when equipment is customized or has a long delivery cycle. | Payment schedule, retention terms, bank details verified through an independent channel, and conditions for releasing each milestone. |
| Warranty coverage | Review the warranty period, covered assemblies, exclusions, response time, travel costs, consumables, and conditions for maintaining coverage. | Furnace ownership cost depends heavily on support for pumps, controls, sensors, heating elements, seals, and hot-zone components. | Detailed warranty clause, service-response commitment, spare-parts pricing, troubleshooting process, and warranty-claim procedure. |
| After-sales service | Assess remote support, local service capability, commissioning support, operator training, preventive-maintenance guidance, and software support. | Fast technical assistance reduces downtime and helps operators achieve stable production sooner. | Service organization chart, response-time commitment, training agenda, remote-access method, and escalation procedure. |
| Total cost of ownership | Evaluate purchase price together with energy use, cooling-water demand, pump maintenance, graphite consumption, spare parts, labor, downtime, and disposal costs. | The lowest initial quotation may not provide the lowest cost per accepted batch. | Five-year cost model, estimated utility consumption, consumables list, maintenance intervals, replacement-part prices, and expected cycle output. |
| 5. Recommended Buyer Scoring Model |
| Technical fit | Suggested weight: 30%
Temperature, vacuum, atmosphere, pressure, uniformity, capacity, and cycle compatibility. | Prevents a low price from compensating for an unsuitable process design. | Score only after reviewing drawings, test data, and written technical guarantees. |
| Quality and compliance | Suggested weight: 20%
Quality system, safety design, documentation, FAT method, and destination-market requirements. | Reduces operational, regulatory, and commissioning risk. | Verify certificates, inspection records, risk assessments, and signed acceptance criteria. |
| Service capability | Suggested weight: 20%
Commissioning, training, spare parts, remote support, response time, and local coverage. | Strong service support protects production continuity after installation. | Use contractual service levels and obtain customer references for comparable equipment. |
| Commercial value | Suggested weight: 20%
Equipment price, installation cost, delivery, utilities, maintenance, consumables, and lifecycle cost. | Creates a more accurate comparison than comparing purchase prices alone. | Compare suppliers using the same scope, Incoterm, currency, warranty, and payment assumptions. |
| Delivery and project risk | Suggested weight: 10%
Schedule credibility, customization risk, component availability, FAT readiness, and logistics plan. | Helps buyers select a supplier that can meet the required production-start date. | Require milestone dates, delay remedies, document-submission deadlines, and a formal change-control process. |